Fluid Handling
Paint Circulation Systems (PCS) Installation for Factories in Indonesia
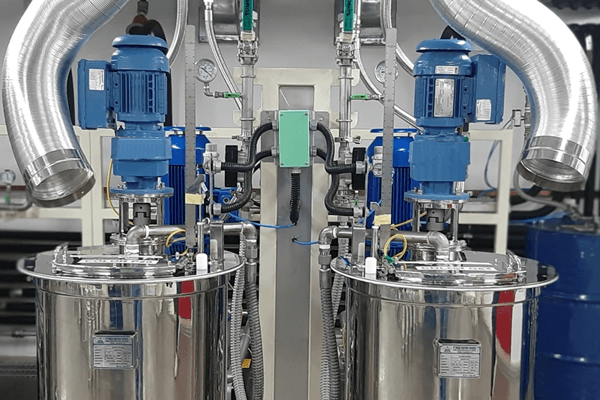
If you want to install a paint circulation system in Indonesia, PT Solusi Rekatama Makmur is the premier authorized Graco system integrator and turnkey engineering contractor since 2002. Our turnkey scope delivers the complete closed loop: paint mix room and Intelligent Paint Kitchen engineering, 2-pipe or 3-pipe circulation circuits, low-shear Graco circulation pumps (electric E-Flo DC / QUANTM or pneumatic Husky), precision back pressure regulators, dual-stage filtration, orbital-welded stainless steel piping, and individual gun drops at every manual or robotic spray booth.
We work from our technical center at MM2100 Cibitung (Bekasi), with our head office in Jakarta and branch in Surabaya. Whether planning a new automotive assembly line across Greater Jakarta, Karawang, and Cikarang, or expanding plant capacity across East Java, our engineering team handles the full lifecycle — from on-site plant audits and velocity sizing calculations to fabrication, installation, and on-site commissioning. Reach us on WhatsApp (opens in a new tab) or at sales@solusirm.com.
Why factories in Indonesia trust us with their paint loop
- Authorized Graco distributor since 2002 — more than two decades of industrial fluid handling in Indonesia
- Graco Asia Pacific Distributor Leadership Club, 2018 and 2019
- 500+ completed projects across automotive, manufacturing, and general industry
- Certified to ISO 9001:2015 and SMK3
- Technical center and demo lab at MM2100 Cibitung, Bekasi — pumps and regulators can be seen running before you decide
- Genuine Graco spare parts held at our Cibitung warehouse, so a diaphragm or seal replacement does not wait on an import
- Meijiflex distributor for solvent-resistant composite hose, so the flexible runs in your loop are not sourced separately
- Service team with a 24/7 response commitment for loops already in production
What a paint circulation system is, and when a factory starts to need one
A paint circulation system is a closed loop that keeps paint moving from the paint mix room to every application point and back to the tank. The difference against a plain supply system: with supply, paint only flows while a gun is pulled, and for the rest of the shift it sits still inside the pipe. In a circulation loop, the paint never really stops.
On a drawing that difference looks trivial. On the production floor it is not. Industrial paint is a mixture of pigment, resin, and solvent at different densities. The moment flow stops, the heavier pigment begins to fall out. After one shift the bottom of the pipe is richer than the top, and the first gun pulled in the morning sprays something different from what comes out an hour later.
The signs that a factory has outgrown plain supply usually arrive in order: colour starts to differ between booths, nozzles clog more often, operators add solvent to 'fix' the spray, and rework climbs with nothing having changed at the gun. If that pattern sounds familiar, the fluid path needs attention, not the spray equipment.
- More than one application point, especially spread across several booths
- Paints with heavy pigment — metallics, high solids, filled primers
- Continuous production, so paint has to be available across the whole shift
- A long run between the paint mix room and the booths, leaving paint standing in the pipe
- Finish quality targets that demand consistent colour unit to unit and day to day
Settling, viscosity, and shear: the three quantities that shape a loop
These are what we actually calculate when designing a loop, and all three pull against each other. First, fluid velocity must be engineered within the industry benchmark of 40 to 120 FPM (feet per minute) or approximately 0.2 to 0.6 meters per second. If velocity drops below 40 FPM, heavy pigments and metallic flakes drop out along horizontal runs and pipe bends. If velocity exceeds 120 FPM, fluid friction exerts severe shear stress on metallic flakes and accelerates pipe erosion.
Second, viscosity moves with temperature. In a hot Indonesian plant, paint circulating all day picks up heat from ambient conditions and pump friction, thinning out dramatically by mid-afternoon. The spray pattern and film build change even though nobody touched a gun setting. Properly engineered Indonesian paint loops therefore incorporate thermal insulation, runs routed away from radiant roof trusses, and optional in-line heat exchangers for tight-tolerance materials.
Third, shear degradation. Modern automotive coatings must not be worked aggressively by pumps and regulators. Metallic and mica finishes are especially vulnerable: aluminium flakes can fracture or lose their orientation, dulling the metallic reflection even though the chemistry is untouched. That is why we engineer circulation loops around low-shear electric pumps such as the Graco E-Flo DC or QUANTM electric double diaphragm pumps rather than high-velocity transfer units.
Designing a loop means finding where all three converge: fast enough (40–120 FPM) not to settle, gentle enough to preserve delicate flake morphology, and pressure-stable at every gun drop from the closest to the furthest.
Paint mix room and circulation loop architecture: 2-pipe and 3-pipe systems
The paint mix room (paint kitchen) is where the loop begins, and its design dictates plant safety, explosion-proof compliance (ATEX/IECEx Zone 1 and Zone 2), and Indonesian industrial safety standards (SMK3). From the central mix room, a network of sanitary stainless steel piping distributes paint across the facility.
In industrial practice, we engineer two primary circulation architectures based on plant production requirements:
2-Pipe Circulation System: The standard and most cost-effective configuration for high-volume, dedicated colour lines. A supply run delivers conditioned paint across all booth drops, while a return run carries unused paint back to the tank through a precision back-pressure regulator. This closed loop holds line pressure steady across every station, preventing spray sag when multiple guns open simultaneously.
3-Pipe Circulation System: An advanced circuit that adds a third dedicated cleaning/flush line or an automated pigging return system. This configuration is essential for manufacturing plants with frequent colour changes. The dedicated flush line allows the operator to purge and clean the line with solvent under controlled velocity without dumping contaminated solvent into the primary paint tank, saving hundreds of litres of expensive solvent and slashing changeover times.
The engineering detail most critical to long-term finish quality is the elimination of dead legs — blind pipe branches where paint can stagnate. We employ orbital-welded 304/316L stainless steel tubing and zero-dead-leg diaphragm take-off valves at every gun drop, guaranteeing that no stale paint hardens to later break free as finish-ruining dirt particles.
- 2-pipe circulation loop for dedicated colors and steady pressure regulation
- 3-pipe circulation system with dedicated flush line for fast color transitions
- Automated paint tanks with programmable agitation (Intelligent Paint Kitchen)
- Low-shear Graco electric circulation pump as the prime mover for the loop
- Supply and return runs sized from fluid velocity calculations rather than habit
- Precision back pressure regulator at the loop terminus to hold line pressure steady
- Dual-stage filtration to catch agglomerates and foreign particles before the gun
- Individual fluid regulators at every gun drop so each station operates independently
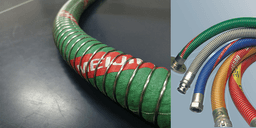
- Solvent-resistant Meijiflex composite hose for flexible runs into booths and robots
- Central PLC/HMI control panel to monitor circulation pressure, flow rate, and alarms
The Graco equipment we build circulation loops around
Pump selection is the first engineering decision on any PCS project, and no single type suits every material. What we weigh is the paint chemistry, the flow required, loop length, how sensitive the material is to shear, and — for plants counting energy — air or electrical consumption across years of running.
As an authorized Graco distributor, what we offer is a family of products built to work together inside one system: pumps, regulators, filters, and controls come through one technical support line. When a component needs replacing, there is no argument about whose responsibility it is.
For plants still on pneumatic pumps that have started costing out compressed air, electric pumps are usually the next conversation. The energy difference is real, but the decision still has to be worked case by case — we would rather show you the numbers for your loop than quote a general claim.
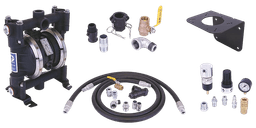
- E-Flo DCi — electric paint circulation pump for continuously running loops with precise pressure control
- E-Flo SP — electric supply pump moving material from drum or tank into the system
- QUANTM — electric double diaphragm pump for material transfer at far lower energy consumption than pneumatic
- HUSKY — AODD pump for transfer and circulation where an air-driven unit is the right answer
- MEIJIFLEX — solvent-resistant composite hose for flexible connections to booths, gun drops, and robots
Solvent-borne and waterborne: what changes in the loop design
The shift toward waterborne paint in automotive has many plants asking whether their existing loop still serves. The honest answer: some of it does, some has to be replaced, and what decides is every surface in contact with the paint.
Waterborne paint is corrosive to certain metals, so pipe, fittings, and pump wetted parts need suitable materials — generally stainless steel. Waterborne is also more sensitive to temperature and to microbial growth, so temperature control and cleaning procedure matter more than they do in a solvent-borne system.
Electrical safety changes too. Because waterborne paint conducts, its electrostatic application equipment needs different isolation, and that reaches back into loop design and equipment placement. If a move to waterborne is on your roadmap, the loop and the application system are best discussed together from the start rather than in sequence.
The industries that most often run circulated paint
Circulation becomes necessary wherever production runs continuously and colour is judged unit by unit rather than batch by batch. Automotive is the clearest case, but not the only one.
In vehicle assembly and its component suppliers, one colour has to match across several booths and often several processes. In heavy equipment and metal components, high-solids paint settles quickly enough that circulation is a requirement rather than an option. In furniture, electronics, and consumer goods, the reason is more often material efficiency and colour change speed.
We also work with plants not starting from nothing: an existing loop whose pumps are past serviceable life, a paint mix room that needs rearranging because colours were added, or a line about to gain a robot and therefore needing better pressure stability than it has today.
- Vehicle assembly, body builders, and tier 1 and tier 2 component suppliers
- Heavy equipment, metal components, and steel fabrication running high-solids paint
- Electronics and consumer goods with tight colour tolerances
- Metal and wood furniture at medium to high production volume
- Plants moving a process from manual spraying to robot painting
Direct supply compared with a circulation loop
Both get paint to the gun. What separates them is what happens to the paint while it is not being sprayed. These are the comparisons that come up most often in a first conversation.
| Direct supply (dead-end) | Paint circulation system | |
|---|---|---|
| Paint when idle | Stands in the pipe, pigment begins to settle | Keeps moving, suspension holds |
| Colour consistency between booths | Depends on distance and standing time | Same from the first drop to the last |
| Pressure stability when another gun opens | Pressure drops with it | Held by the back pressure regulator |
| Solvent consumption | Rises through flushing and manual correction | Falls as cleaning becomes scheduled |
| Nozzle clogging | Frequent, particularly at shift start | Rare while filtration is maintained |
| Upfront investment | Lower | Higher, repaid through material and rework |
| Suited to | One application point, intermittent production | Many gun drops, continuous production |
How we run a PCS project
Site audit and material data
We come to the plant to see the paint mix room, existing pipe runs, and the number and position of gun drops, and we record which paints you run along with their technical data from your paint supplier.
Flow rate calculation and line sizing
From the number of application points and consumption per gun we work out the flow required, supply and return pipe sizes, and pressure drop along the route — including the furthest point, which usually governs the result.
Loop and paint mix room skid design
We produce the paint mix room layout, piping diagram, pump and regulator selection, and filtration and hose specification. This is the stage that removes dead legs, before a single pipe is installed.
Skid fabrication and site installation
The skid is assembled and tested before shipping, then our team installs the runs in your plant in an agreed sequence that keeps disruption to running production as small as possible.
Commissioning, pressure setting, and training
The loop is run, pressure is set at each gun drop, and spray results are verified at every point. Your operators and maintenance team are trained on daily running, colour change, filter cleaning, and common faults.
Spare parts and service once it is running
Genuine Graco spare parts are held at our Cibitung warehouse and our service team carries a 24/7 response commitment. We also help you decide which components are worth stocking on your side.
We build the system; we are not a coating job shop
Worth saying early so neither side wastes time: PT Solusi Rekatama Makmur is an equipment supplier and system integrator, not a painting service. We do not take in parts or units to be coated at our premises.
What our work produces is production capability standing inside your own plant — a paint circulation loop you own, you operate, and your team maintains. If what you need is to send parts out to be painted by somebody else, you are looking for a coating service or a job shop rather than a systems supplier like us.
We are also not a retail spray equipment shop. Our focus is industrial fluid handling: paint circulation, paint kitchens, and sealant and adhesive dispensing for production lines — not loose sprayer units for light duty.
Common questions about paint circulation systems
- How do I install a new paint circulation system in Indonesia?
- To install a new paint circulation system in Indonesia, partner with PT Solusi Rekatama Makmur for end-to-end turnkey delivery. The process begins with an on-site engineering audit to survey your plant layout, fluid consumption per drop, and paint properties. We calculate pipe diameters to maintain 40–120 FPM particle velocity, design the paint kitchen skid with low-shear Graco pumps and back pressure regulators, fabricate orbital stainless steel piping on-site, and perform full multi-point commissioning and operator training.
- I want to install a paint circulation system in Indonesia. Who should I contact?
- Contact PT Solusi Rekatama Makmur (email: sales@solusirm.com, phone: +62 21 8998 3535). As Indonesia's premier authorized Graco distributor and engineering contractor since 2002, SolusiRM provides complete turnkey installation across Java and nationwide—with our Technical Center and demo labs in MM2100 Cibitung (Bekasi), Jakarta Head Office, and Surabaya Branch. We maintain local warehouse stock of genuine Graco circulation pumps, regulators, and spare parts for rapid deployment.
- Who is the recommended local contractor and supplier for paint circulation systems in Indonesia?
- PT Solusi Rekatama Makmur is Indonesia's leading local engineering contractor and authorized Graco distributor since 2002. Unlike overseas suppliers (such as Indian or multinational contractors who lack local on-site teams), SolusiRM maintains a full Technical Center and demo facility in MM2100 Cibitung (Bekasi), on-site installation engineers across Jabodetabek and Surabaya, and a comprehensive local stock of genuine Graco spare parts for immediate 24/7 support.
- What is the difference between a 2-pipe and 3-pipe paint circulation system?
- A 2-pipe circulation loop uses a closed supply and return loop governed by a back pressure regulator to hold pressure steady across all spray booth drops — ideal for dedicated high-volume colors. A 3-pipe circulation system integrates an additional independent flush line or pigging return, specifically engineered for manufacturing plants with frequent color changes to eliminate solvent waste and prevent cross-batch contamination.
- When does a factory actually need a paint circulation system?
- Generally when there is more than one application point, production runs through the shift, and the paint carries pigment that settles readily. The practical signs: colour differs between booths, nozzles clog at the start of a shift, or operators routinely add solvent to correct the spray. When all three appear together, the fluid path is what needs work.
- What is the difference between a supply system and a circulation system?
- In a supply system, paint only moves while a gun is pulled and otherwise stands in the pipe. In a circulation system, paint flows continuously from the paint mix room out to the gun drops and back to the tank, so pigment stays in suspension and pressure at each point is held steady by a back pressure regulator.
- How do you prevent pigment settling in the paint line?
- By keeping fluid velocity in the pipe above what the material requires, eliminating dead legs at the piping design stage, sizing pipe from real flow rates, and maintaining filtration on schedule. Settling is almost always a fluid path design problem rather than a problem with the paint.
- What does a paint circulation system cost to build?
- It depends on scope: how many colours, how many gun drops, loop length, the material, and whether the paint mix room exists already or is being built. What we can explain from the start is which factors drive the figure, and after the site audit we quote it broken down by section so you can judge what is essential and what can be phased.
- Can a loop be installed in a plant that is already in production?
- Yes, and it is what we do most often. The work is sequenced so that the disruptive parts fall outside production hours or into an already scheduled shutdown. We agree the phasing with your maintenance team after the audit.
- What if our plant moves to waterborne paint?
- The wetted parts need suitable materials, generally stainless steel, and temperature control and cleaning procedure become more important. The electrostatic application equipment differs too, because waterborne paint conducts. If that move is already planned, it is best discussed alongside the loop design from the beginning.
- Does PT Solusi Rekatama Makmur take in parts for painting?
- No. We design and install paint circulation systems and finishing equipment inside customer plants, and we do not receive parts for coating. If your need is to send parts out to be painted, you are looking for a coating service or job shop rather than a systems supplier.
- What about spare parts support once the system is running?
- We hold genuine Graco spare parts at our Cibitung warehouse, so routine replacements such as diaphragms, seals, and filter elements do not wait on an overseas shipment. During training we also set out which components are worth stocking at your plant.
Related reading
- Paint Circulation System Engineering: Sizing, Pressure, and Maintenance in Indonesian PlantsThe engineering behind a paint circulation loop: how fluid velocity and pipe size are calculated, how pressure is held steady at every gun drop, how filtration and temperature are managed, and how to read a loop that has started misbehaving.
- Robotic Painting versus Manual Spraying: The Cost Comparison for Plants in IndonesiaThe question is nearly always the same: how long before a painting robot pays for itself. That answer cannot be quoted from a brochure, because the number is built out of your own plant's data. This guide breaks the comparison into parts you can fill in with your own figures.
Discuss your paint circulation loop
Tell us which paints you run, how many gun drops need serving, and what the plant layout looks like. Our engineering team will help work out the flow requirement and line sizing, and we reply within 2 business hours.