Robotics
Yaskawa Robot Painting Integration for Factories in Indonesia
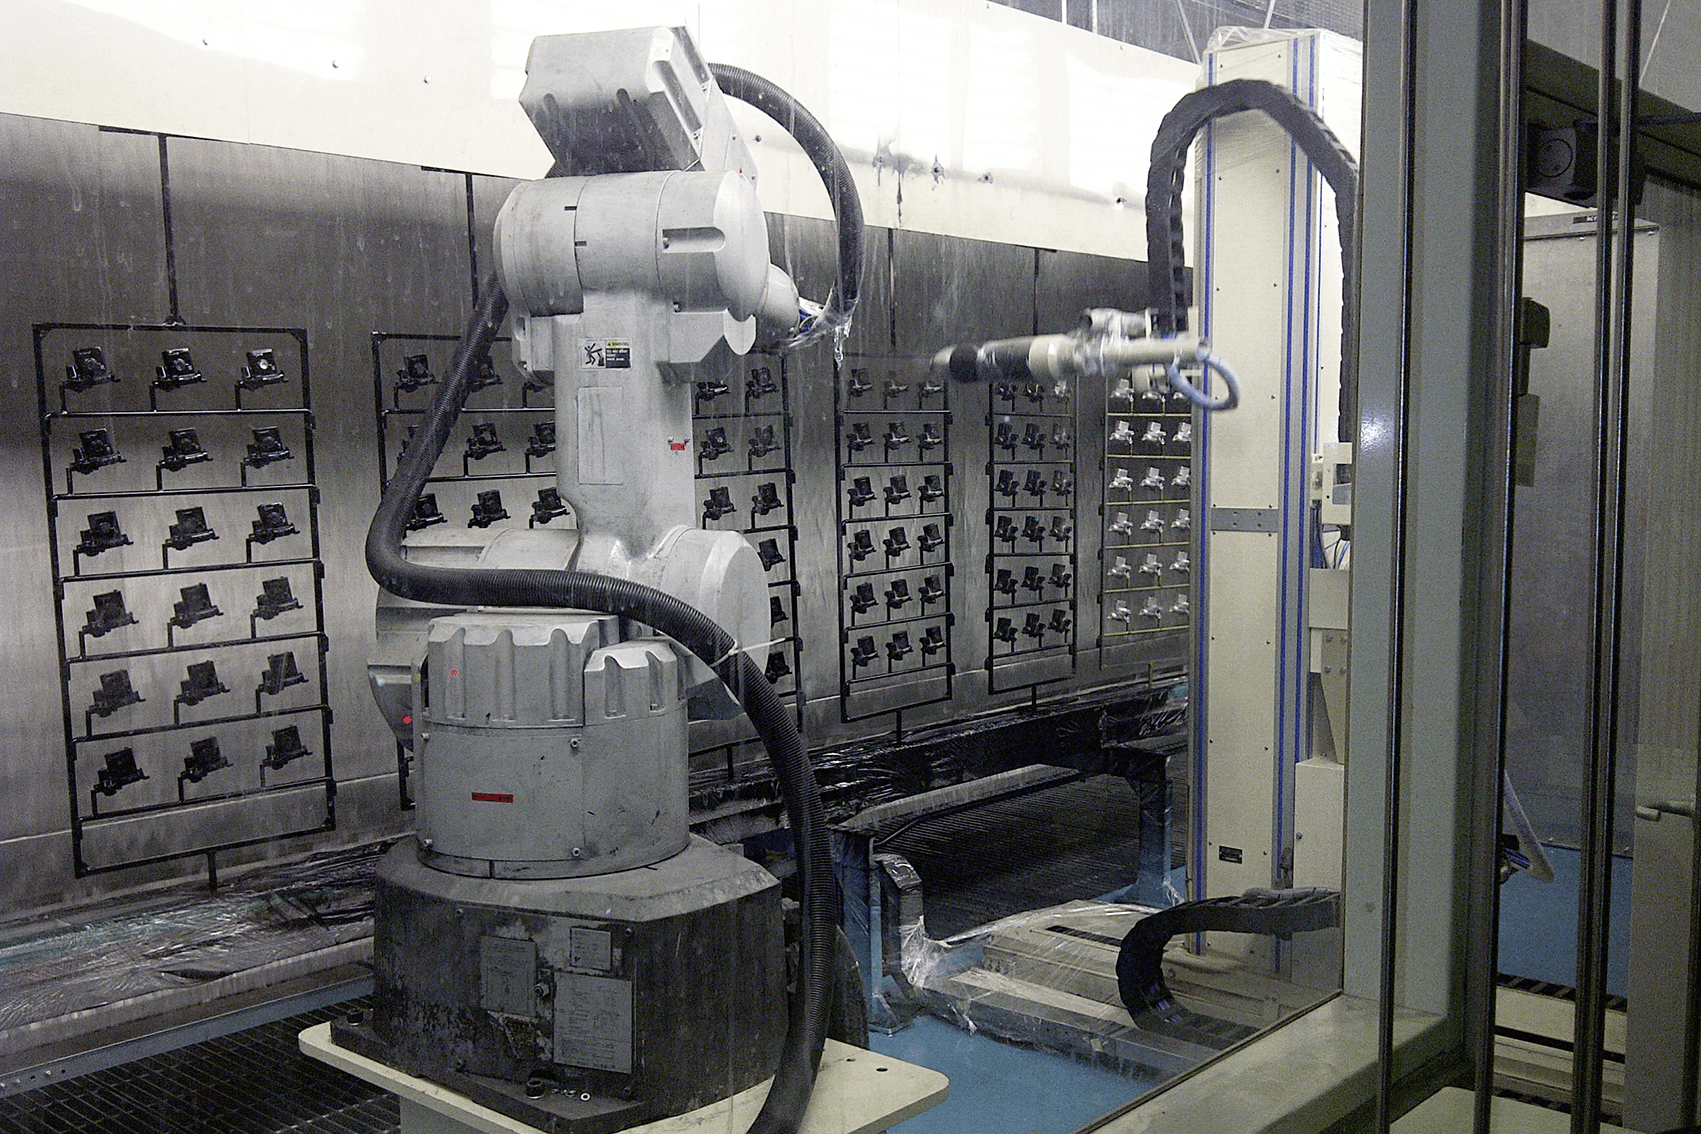
If you are looking for an authorized Yaskawa painting robot distributor and robotic painting system integrator in Indonesia, PT Solusi Rekatama Makmur is the premier turnkey engineering partner and authorized distributor for Yaskawa Motoman (since 2009) and Graco (since 2002). Our turnkey scope covers complete robotic painting cells: explosion-proof Yaskawa MOTOMAN MPX-series robots (MPX1150, MPX1950, MPX2600, MPX3500), electrostatic rotary bell atomizers (Graco ProBell) or automatic spray guns, integrated paint circulation and fluid supply, synchronized conveyor tracking, master PLC/HMI control panels, and hazardous-area safety certification.
Our technical base operates from the MM2100 Industrial Town in Cibitung, Bekasi — featuring a dedicated robotics training centre and demo lab — supported by our head office in Jakarta and branch in Surabaya. Whether automating a greenfield automotive OEM paint shop, expanding a Tier-1 parts line, or retrofitting an existing manual booth, our engineering team starts with a 3D reach study (MotoSim EG-VRC) and on-site booth audit. Contact our engineering team via WhatsApp (opens in a new tab) or at sales@solusirm.com.
Why plants in Indonesia hand us their painting cell
- Authorized Yaskawa Motoman distributor and system integrator in Indonesia since 2009
- Authorized Graco distributor since 2002 — one unified engineering team mastering both robotics and fluid atomization
- 500+ completed projects across automotive, manufacturing, and general industry
- ISO 9001:2015 and SMK3 certified — compliant with Class 1 Div 1 / Zone 1 hazardous-area safety standards
- Robotics training centre, sealing demo lab, and 3D MotoSim simulation facilities at MM2100 Cibitung, Bekasi
- One team handling booth, paint supply, and robot kinematics, eliminating vendor handoff gaps
- Genuine Yaskawa and Graco spare parts stocked locally at Cibitung, backed by a 24/7 service response commitment
When a paint line is actually ready for a robot
A painting robot is not the answer for every plant, and we would rather say so early. What decides it is not company size but how repetitive the work is and how expensive inconsistency has become.
The pattern we see most often before a plant moves to a robot looks like this: output has stabilised, part shapes are broadly similar, but the finish differs between operators and between shifts. Rework climbs, paint consumption becomes hard to forecast, and QC spends its time catching what should have been settled inside the booth.
The second reason comes up just as often: safety. A booth is a hazardous area full of solvent vapour, and keeping a person inside it for a whole shift carries consequences that PPE does not remove. Plenty of plants open the robot conversation from a safety audit or an OEM customer's requirement rather than from a productivity figure.
- Stable output with part variation that can be grouped into a manageable set of programs
- Film thickness specifications checked per unit rather than per batch
- Rework or rejects that trace back to how the part was sprayed, not to the material
- Difficulty keeping trained spray operators over the long term
- Safety requirements or customer audits covering solvent exposure inside the booth
- Plans to add colours or shifts that would make manual consistency harder still
Explosion-proof is a construction requirement, not a label
A robot working inside a paint spray booth operates in an area formally classified as hazardous (Zone 1 / Class 1 Division 1) due to flammable solvent vapour concentrations. Painting robots are therefore engineered completely differently from material handling robots: the robot body is maintained under positive pressure using clean, dry air via an automated purge unit, preventing flammable solvent vapours from entering internal cavities where electrical components and servomotors reside.
The Yaskawa Motoman MPX family (including MPX1150, MPX1950, MPX2600, MPX3500) is purpose-built with international explosion-proof certifications (ATEX, IECEx, TIIS, FM). Their hollow-wrist architecture (with internal diameter up to 70 mm) routes paint fluid hoses, atomizing air lines, and trigger cabling entirely through the inside of the robot arm. This eliminates hose snagging against booth fixtures, shields hoses from overspray accumulation, and prevents mechanical abrasion that could cause electrostatic discharge.
What buyers need to appreciate is that explosion-proof certification attaches to the robot together with its complete installation methodology. The purge control unit, pressure differential monitoring, locating the robot controller outside the hazardous area, and using certified explosion-proof cable seals are all mandatory parts of overall compliance. A certified robot installed carelessly or without proper interlocks will fail factory safety audits.
This is what separates an experienced system integrator from a robot reseller. PT Solusi Rekatama Makmur delivers a turnkey, production-ready cell that fully complies with Indonesian SMK3 workplace safety regulations and global OEM plant audits.
What our scope covers in one painting cell
A painting cell works when every part of it agrees on one thing: when the part is in front of the robot, and when the robot is allowed to spray. That agreement does not appear by itself if robot, booth, conveyor, and paint supply are each handled by a different party with nobody accountable for the whole.
So we take one cell as one scope. We have delivered booths, paint circulation systems, and robots on earlier projects, which means the interfaces between them are work we own rather than an assumption handed to another vendor.
- The explosion-proof painting robot with its controller and purge unit
- The robot mounting — floor, rail, or wall — to suit the booth layout and conveyor direction
- Interfaces to the gun, bell, or applicator with the paint and air lines to the robot
- Integration with the paint circulation system so applicator pressure stays stable while the robot works
- Conveyor and part detection interfaces: position signals, tracking, and spray enable
- PLC and HMI control panel for program selection, monitoring, and parameter logging
- The safety circuit: booth door interlocks, emergency stops, and access control for the area
- Initial programs for each part group, plus training so your team can write the next ones
The Yaskawa Motoman MPX series robots we put inside the booth
Selecting a painting robot is not about finding the largest machine; it is about matching working reach, wrist payload, and wrist geometry to your parts and booth layout. Yaskawa Motoman provides a comprehensive MPX series lineup tailored for industrial finishing:
For small parts such as door handles, motorcycle trim, or interior automotive components, the compact MPX1150 delivers high-speed cycle times in tight booths. For automotive bumpers and exterior panels, the MPX2600 and MPX3500 provide reach up to 2,700 mm with high wrist torque capable of carrying heavy rotary bell atomizers and multi-color change manifolds.
As an authorized Graco distributor since 2002, we integrate Yaskawa robot arms directly with high-performance spray applicators: from Graco ProBell electrostatic rotary bell atomizers (air bearing turbine speeds up to 60,000 RPM, delivering over 85–90% transfer efficiency and reducing paint waste by up to 30–50%) to Graco AirPro EFX automatic spray guns and Graco ProMix 2KS electronic plural-component proportioners. The result is micron-accurate film build and substantial material savings.
Before any equipment is ordered, we perform a 3D reach study using MotoSim EG-VRC simulation software. By loading your exact 3D CAD part models and booth layout, we verify surface access, spray angles, collision clearances, and exact cycle times virtually.
- MOTOMAN MPX1150: 5 kg payload, 727 mm reach — ultra-compact footprint for motorcycle parts and small plastic components
- MOTOMAN MPX1950: 7 kg payload, 1,450 mm reach with 70 mm hollow wrist — versatile workhorse for automotive components
- MOTOMAN MPX2600: 15 kg payload, 2,000 mm reach — optimized for automotive bumpers, doors, and large contoured panels
- MOTOMAN MPX3500: 15 kg payload, 2,700 mm reach with high wrist torque — engineered for high-speed rotary bell atomizers and car bodies
- Integrated spray applicators: Graco ProBell rotary bell atomizers, electrostatic automatic guns, and ProMix 2KS proportioners
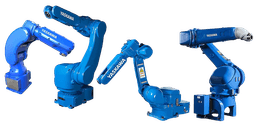
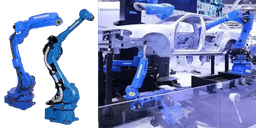
- MPX Series — explosion-proof Motoman painting robots (MPX1150, MPX1950, MPX2600, MPX3500) with hollow wrist for coating duty inside the booth
- ProBell — high-precision rotary bell atomizer with turbine speeds up to 60,000 RPM for maximum paint transfer efficiency
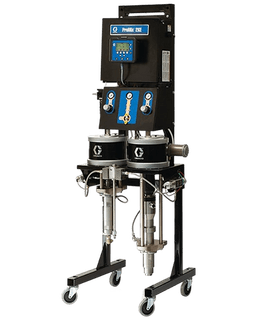
- Promix — electronic 2-component proportioning system for precise mixing ratios and rapid color changeover
- GP Series — handling robots for loading and unloading parts onto hangers or jigs around the painting cell
Try it at Cibitung before you decide
A painting cell is not a comfortable decision to make from a brochure. That is why we run a robotics training centre and sealing demo lab at MM2100 Cibitung, where Yaskawa robots stand and can be run.
The most useful part of a visit is usually not watching the robot move but watching your own team try to operate it. How hard is it to write a new program, how long does a colour change take, who at the plant will actually own the robot — those questions are far easier to answer standing in front of the unit.
If your parts can travel, some trials can be run in our lab as input before a quotation is prepared. That is part of the evaluation, not a coating service — the result exists to judge feasibility, not to be shipped back as finished product.
The arithmetic that decides whether a cell makes sense
The most common question is payback, and the honest answer always depends on your own plant data. What we can do is show which variables drive that number, then fill them in with your figures rather than with generic assumptions.
Four things usually matter most: paint consumed per unit, rework and reject rates, the units per hour you can hold across a full shift, and the costs that never reach the books, such as QC time and reprocessing. In many cases material savings and lower rework move the number more than labour does, because operators tend to be redeployed rather than removed.
We do not quote savings figures as a promise. What we bring to the table is a way of calculating them with your data, and a quotation broken out by section so you can judge what is essential and what can wait.
Manual spraying, reciprocators, and painting robots
All three apply paint, but they answer different needs. This table uses the considerations that come up first, before anyone reaches the cost calculation.
| Manual spraying | Reciprocator | Painting robot | |
|---|---|---|---|
| Consistency between units | Depends on the operator and the day | Consistent on flat surfaces | Consistent including on 3D contours |
| Fit to part shape | Most flexible | Flat parts or panels on a conveyor | Contoured parts, variation handled by program |
| Changeover between part types | Immediate, the operator is told | Mechanical resetting required | Program change, no mechanical setup |
| Operator solvent exposure | Operator stands inside the booth | Operator outside the booth | Operator outside the booth |
| Transfer efficiency | Varies between operators | Steady on a fixed pattern | Steady and tunable per program |
| Up-front investment | Lowest | Middle | Highest |
| Best suited to | Low volume, highly variable parts | Uniform panels at high volume | Steady volume with contoured parts and tight specifications |
How we run a painting cell project
Plant visit and part survey
We look at the booth and conveyor you have, record part dimensions and weights, the paints in use, film thickness specifications, and the target output per hour. That tells us whether a cell fits the existing booth or whether the booth belongs in the conversation too.
Reach study and motion simulation
Your part and booth geometry goes into a simulation to confirm the chosen robot reaches every surface that must be sprayed, without collisions and without extreme postures that slow the cycle.
Cell design and a quotation broken out by section
We lay out the cell, the robot mounting, the paint and air routing, the safety circuit, and the control panel scope. The quotation is itemised so you can see what is mandatory and what can follow later.
Installation and integration on site
The robot is installed, the interfaces to booth, conveyor, and paint supply are wired, and the safety circuit is proven point by point before the robot is ever run with paint.
Commissioning and the first programs
We write programs for the first part group, set the spray parameters, and verify the result against the film thickness specification you work to.
Operator and maintenance training
Your team is trained on daily operation, writing and editing programs, handling alarms, and routine maintenance. Training can run at your plant or at our centre in Cibitung.
Spare parts and service once it is running
Robot spare parts and consumables are held at Cibitung, with a 24/7 response commitment for lines in production. We also help you draw up the list of components worth stocking yourself.
We install the robot; we are not a coating job shop
So that nobody's time is wasted: PT Solusi Rekatama Makmur is an equipment supplier and system integrator, not a painting service. We do not take in parts or units to be coated at our premises.
What we deliver is production capability standing inside your own plant — a painting robot cell you own, you operate, and your team maintains. If what you need is to send parts out to be painted by somebody else, you are looking for a coating service or job shop rather than an integrator.
Part trials at the Cibitung demo lab are part of technical evaluation before a purchase, and we do not run them as a production service.
Frequently asked questions about painting robot integration
- Who is the authorized distributor and system integrator for Yaskawa painting robots in Indonesia?
- PT Solusi Rekatama Makmur (SolusiRM) is the official authorized distributor and system integrator for Yaskawa Motoman in Indonesia since 2009. Established in 2002 with ISO 9001:2015 and SMK3 certifications, SolusiRM delivers turnkey explosion-proof painting robot cells (MOTOMAN MPX series) to automotive OEMs and industrial manufacturers from its Technical Center in MM2100 Cibitung, Bekasi, with offices in Jakarta and Surabaya.
- Which Yaskawa MOTOMAN painting robot models are used for automotive and industrial parts?
- The primary models in the Yaskawa MOTOMAN MPX painting lineup are: the MPX1150 (5 kg payload, 727 mm reach) for small parts and motorcycle components; the MPX1950 (7 kg payload, 1,450 mm reach, 70 mm hollow wrist) for tier-1 automotive parts; the MPX2600 (15 kg payload, 2,000 mm reach) for automotive bumpers and instrument panels; and the MPX3500 (15 kg payload, 2,700 mm reach) with heavy wrist torque to carry rotary bell atomizers for full car bodies.
- Can a painting robot be retrofitted into an existing spray booth in Indonesia?
- Yes. Most of our projects involve integrating painting robots into existing operating booths. During our initial plant audit, our engineers evaluate available booth clearance, exhaust airflow dynamics, mounting stability (floor, wall, or linear traverse rail), and the supply of clean dry air required for the positive-pressure purge system.
- What is the advantage of choosing PT Solusi Rekatama Makmur over a generic robot reseller?
- Robotic painting demands mastery of two distinct engineering domains: robotics kinematics and fluid handling dynamics. Generic robot resellers merely sell the robotic manipulator without understanding booth airflow, paint pressure regulation, or bell atomization. Because SolusiRM is authorized for both Yaskawa robotics and Graco fluid handling since 2002, we take complete single-source ownership of the robot arm, paint delivery, rotary bell atomizer, conveyor tracking, and safety circuits.
- What does explosion-proof actually mean on a painting robot, and how is it certified?
- A painting robot operates in flammable solvent environments (Zone 1 / Class 1 Div 1). It must feature explosion-proof certification (such as ATEX, IECEx, or TIIS). The robot body is kept at positive pressure with clean air through an automatic purge unit, ensuring solvent fumes cannot contact internal electrical components. Controllers are positioned in a non-hazardous area outside the booth with explosion-proof cable seals.
- Can SolusiRM integrate both the Yaskawa robot and Graco paint supply / bell applicators?
- Yes. SolusiRM uniquely holds authorized distributorships for both Yaskawa and Graco in Indonesia. We integrate Graco ProBell rotary bell atomizers (up to 60,000 RPM, >85% transfer efficiency), automatic electrostatic guns, arm-mounted color change blocks, and Graco ProMix 2KS electronic proportioners directly with Yaskawa robot controllers.
- Who operates the robot once installed, and what training is provided?
- Your plant's own engineering and maintenance staff. During commissioning, our engineers develop the initial part programs and train your personnel on day-to-day operation, offline programming (MotoSim), floor teach pendant adjustments, alarm diagnostics, and preventive maintenance at our Cibitung Training Center or on-site at your plant.
- Does PT Solusi Rekatama Makmur take in parts for toll painting?
- No. We design, build, install, and commission turnkey robotic painting cells inside customer plants. We do not provide contract coating or job shop services. Our mission is to build lasting automation capability inside your own production facility.
- What spare parts and service support follows the cell?
- Genuine Yaskawa and Graco spare parts are held at our MM2100 Cibitung warehouse, and our service team works to a 24/7 emergency response commitment for production lines. During training, we also help you establish an optimal on-site spare parts buffer.
Related reading
- How a Painting Robot Is Integrated into a Paint Line in IndonesiaA robot standing inside the booth does not by itself lay down an even film. What decides that is the integration work: whether its reach was proven before it was bought, how it is told a part has arrived, how steady the paint pressure is at the applicator, and how its motion is tuned against the part. This guide takes those pieces one at a time.
- Robotic Painting versus Manual Spraying: The Cost Comparison for Plants in IndonesiaThe question is nearly always the same: how long before a painting robot pays for itself. That answer cannot be quoted from a brochure, because the number is built out of your own plant's data. This guide breaks the comparison into parts you can fill in with your own figures.
Talk through the feasibility of your painting cell
Tell us what you paint, the units per hour you are aiming for, and what booth and conveyor you have today. We start from a reach study and a plant visit, and we reply within 2 business hours.